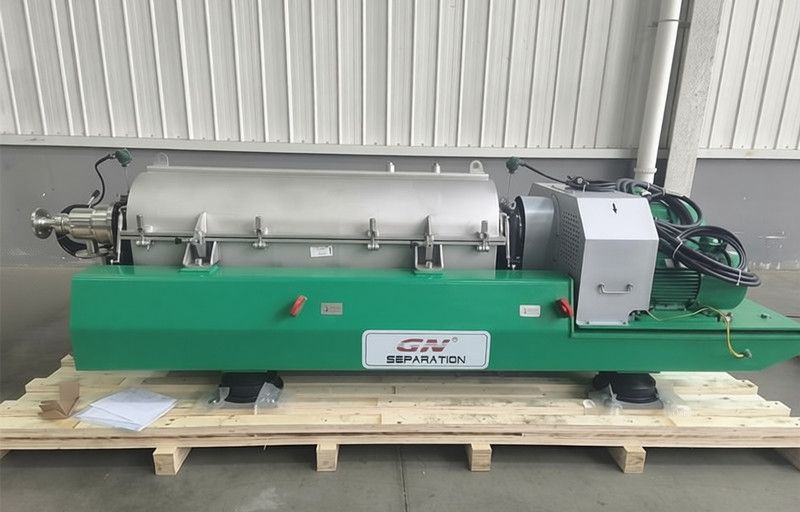
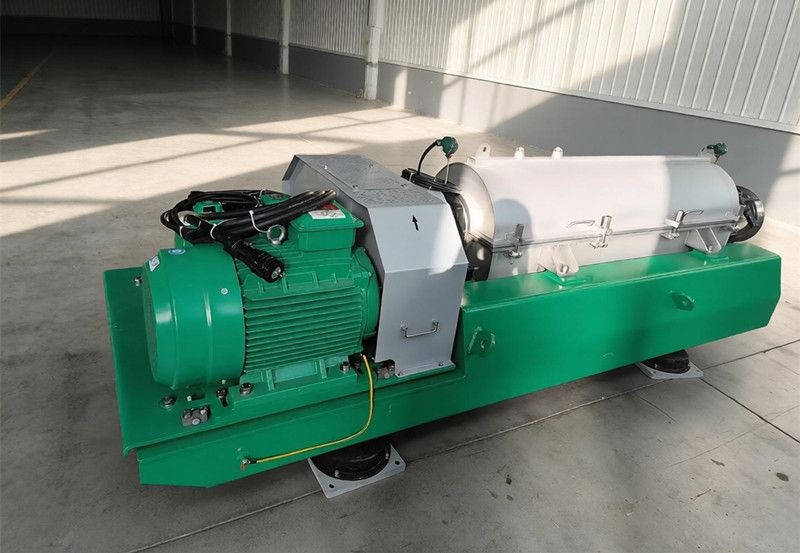
Australia ranks among the world’s major canola‑producing regions, where edible‑oil processors demand robust continuous‑flow separation equipment to purify crude canola oil and remove meal fines, phospholipids and fine solid residues efficiently. GN Solids Control delivered a customized decanter centrifuge solution for one local Australian canola oil processor, bringing stable solid‑liquid clarification performance for their oil‑pressing production line.
As a global manufacturer specializing in decanter and three‑phase centrifuges, GN Solids Control designs separation equipment tailored to diverse industrial requirements. GN covers a full‑size decanter centrifuge portfolio ranging from 9‑inch up to 30‑inch bowl models, alongside full‑hydraulic‑drive versions for tough operating conditions. The in‑house PLC and electrical control department allows GN to optimize automatic monitoring, differential‑speed adjustment and process parameter tuning for different feed materials, greatly boosting equipment stability and uptime.
For this Australian canola‑oil clarification project, GN selected its clarification‑type decanter centrifuge. Key Features:
- Internal screw propeller polishing treatment to avoid material residue and deterioration, meeting hygiene requirements
- The centripetal pump is adopted for flexible adjustment of the depth of the liquid pool without stopping the machine
Operating under high centrifugal force, the unit continuously separates fine meal solids from crude pressed canola oil. It delivers clarified oil for downstream refining while discharging de‑watered solid residues. Compared with traditional static sedimentation tanks, the centrifuge cuts floor occupation, lowers oil loss, and improves overall production throughput, well matching Australia’s strict food‑grade safety standards.
Beyond edible‑oil clarification, GN industrial decanter centrifuges are widely deployed for sludge dewatering, thickening, liquid clarification and three‑phase separation across mining, drilling waste treatment and biodiesel sectors. Supported by GN’s Australia local partner network, the project includes pre‑sales technical simulation, on‑site commissioning and after‑sales spare‑parts supply. This canola‑oil case further proves GN’s capability to adapt its core centrifuge technology from oil‑gas solids‑control to diversified food‑processing industrial separation requirements.